
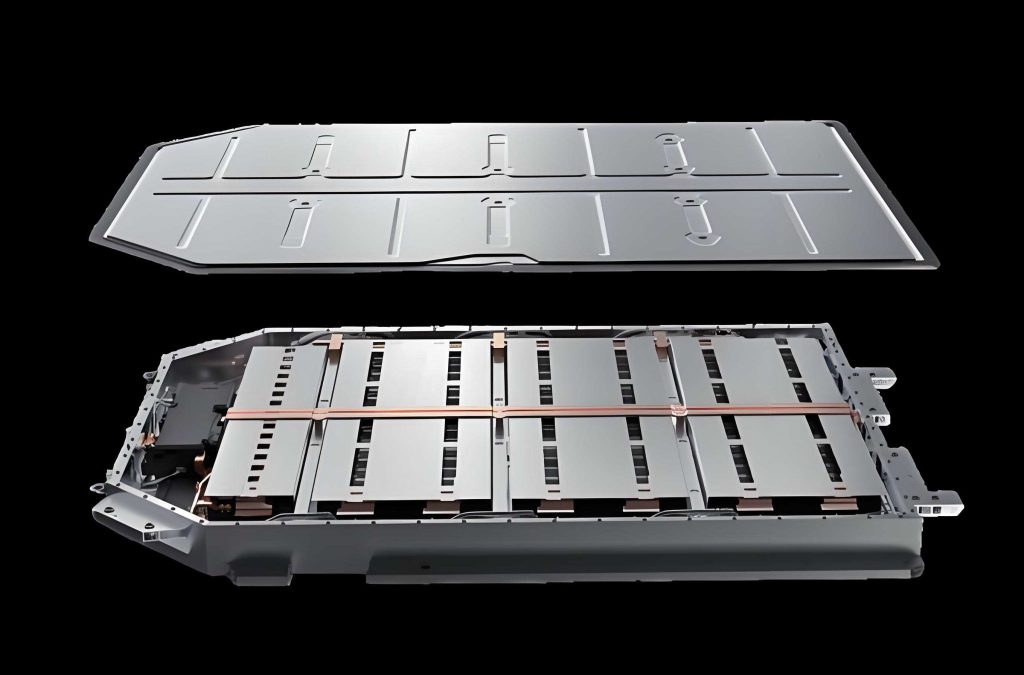
During the past few decades, the progressive depletion of fossil fuels and the continuous deterioration of urban air quality have accelerated the search for clean, renewable and high-efficiency energy-storage devices. Among all the candidate systems, the lithium-ion battery has emerged as one of the most promising electrochemical power sources, because it offers high operating voltage, high energy density, low self-discharge, long cycle life, and no memory effect. Initially, lithium-ion batteries were developed mainly for portable consumer electronics, including mobile phones, laptop computers and digital cameras. More recently, however, the demand for a reliable high-voltage battery system has been extended to electric vehicles, hybrid electric vehicles, and large-scale stationary energy-storage applications. Consequently, the development of large-format lithium-ion power batteries has become the focus of intense research and industrial attention throughout the world.
The most critical bottleneck that restricts the commercial application of electric vehicles is still the performance, cost, and safety of the battery. The power battery used in an electric vehicle must satisfy several demanding requirements: high specific energy to ensure a long driving range; high specific power for rapid acceleration and hill-climbing; excellent charge acceptance for regenerative braking; long calendar and cycle life; wide operating-temperature range; high reliability under abusive conditions; and low production cost. The traditional lead-acid battery and nickel-metal-hydride battery cannot simultaneously fulfil all these requirements. Lead-acid batteries suffer from low specific energy and environmental pollution caused by lead; nickel-metal-hydride batteries have relatively high self-discharge and poor high-temperature behaviour. The lithium-ion battery, in contrast, has several intrinsic advantages, which makes it the most attractive candidate for the next generation of vehicle traction batteries and therefore an ideal basis for a high-voltage battery pack.
The early lithium-ion battery used LiCoO₂ as the positive electrode, a layered graphitic carbon as the negative electrode and a non-aqueous LiPF₆-containing electrolyte. During charge and discharge, lithium ions shuttle between the two electrodes, so the cell is often described as a “rocking-chair” battery. The reactions of a LiMn₂O₄/graphite high-voltage battery can be written as follows:
$$ \text{Positive: } \ \text{LiMn}_2\text{O}_4 \rightleftharpoons \text{Li}_{1-x}\text{Mn}_2\text{O}_4 + x\text{Li}^+ + x\text{e}^- $$
$$ \text{Negative: } \ \text{C}_6 + x\text{Li}^+ + x\text{e}^- \rightleftharpoons \text{Li}_x\text{C}_6 $$
Although LiCoO₂ has been the dominant cathode material in commercial lithium-ion batteries, its application in large-scale high-voltage battery systems is limited by the high price and scarce reserve of cobalt. Moreover, LiCoO₂ tends to release oxygen at elevated temperature, which creates a serious safety concern in large-format cells. LiNiO₂ has a higher specific capacity but suffers from synthesis difficulties and poor thermal stability. The spinel LiMn₂O₄ has received much attention as one of the most promising positive-electrode materials for a high-voltage battery owing to its low cost, abundant manganese resources, environmental friendliness, good safety, and its three-dimensional channel structure that permits fast lithium-ion diffusion. The major disadvantage of LiMn₂O₄ is capacity fading upon cycling, especially at elevated temperature, but this issue can be alleviated by appropriate doping, surface modification and optimization of the manufacturing parameters.
Choosing an advanced electrode material is not, by itself, sufficient to guarantee the performance of a final high-voltage battery. The practical performance of the cell depends strongly upon the manufacturing conditions, such as the mixing formula, the ratio of conductive agent and binder, the electrode density, the electrolyte filling amount, and the formation schedule. Small variations in these process variables can lead to remarkable changes in discharge capacity, internal resistance, rate capability, cycle life and abuse tolerance. Therefore, systematic research on the key manufacturing parameters is indispensable for producing a high-performance and highly safe high-voltage battery. This work focuses on the influence of these parameters on the electrochemical behaviour of LiMn₂O₄ power batteries and attempts to establish a complete processing technology that is suitable for industrial mass production.
The present investigation can be summarized in five major parts:
- Optimization of the mixing formula, especially the mass percentage of active material, conductive carbon black and binder.
- Study of the capacity-balance coefficient between the positive and negative electrodes.
- Determination of the optimum compaction density for both the LiMn₂O₄ cathode and the graphite anode.
- Investigation of the electrolyte filling amount and its influence on discharge capacity, internal resistance and capacity distribution.
- Systematic comparison of formation schedules, followed by the design, fabrication and evaluation of a large-capacity prismatic LiMn₂O₄ high-voltage battery.
1. Technical Background and Requirements for a High-Voltage Battery
1.1 Comparison of power-battery chemistries
The development of electric vehicles has stimulated extensive research on advanced battery systems. Four representative battery chemistries that have been considered for electric traction are compared in Table 1.
| Property | Lead-acid | Ni-Cd | Ni-MH | Li-ion |
|---|---|---|---|---|
| Nominal cell voltage (V) | 2.0 | 1.2 | 1.2 | 3.6–3.8 |
| Specific energy (Wh kg⁻¹) | 30–40 | 40–60 | 60–80 | 120–200 |
| Specific power (W kg⁻¹) | ~200 | 150–300 | 200–1000 | 500–2000 |
| Cycle life | 300–500 | 500–1000 | 500–1000 | 1000–3000 |
| Self-discharge (% per month) | 4–6 | 15–20 | 20–30 | 3–5 |
| Memory effect | No | Yes | Slight | No |
| Environmental friendliness | Poor | Poor | Good | Good |
| Cost | Low | Moderate | High | Moderate to high |
From Table 1, it is clear that the lithium-ion battery provides the highest voltage and the most attractive combination of energy and power densities. For this reason, the lithium-ion high-voltage battery has become accepted as the preferred power source for modern electric vehicles. The design of a large-format high-voltage battery, however, requires strict control of electrode processing because large electrodes amplify the adverse effects of any non-uniformity or defective interface. If the electrode sheet is not manufactured carefully, the resulting high-voltage battery suffers from low material utilization, high internal resistance, short cycle life, and severe safety hazards.
1.2 Positive-electrode materials suitable for high-voltage battery systems
Three main families of lithium transition-metal oxides are relevant to power batteries: layered LiCoO₂, layered LiNiO₂ and its derivatives, spinel LiMn₂O₄, and olivine LiFePO₄. Table 2 compares the typical characteristics of these positive electrode materials.
| Material | Theoretical capacity (mAh g⁻¹) | Practical capacity (mAh g⁻¹) | Voltage plateau (V vs Li/Li⁺) | Thermal stability | Relative cost |
|---|---|---|---|---|---|
| LiCoO₂ | 274 | 140–155 | 3.9 | Poor above 150 °C | High |
| LiNiO₂ | 275 | 190–210 | 3.8 | Poor | Moderate |
| LiMn₂O₄ | 148 | 100–125 | 4.0–4.2 | Good | Low |
| LiFePO₄ | 170 | 130–165 | 3.4 | Excellent | Moderate |
The spinel LiMn₂O₄ is particularly interesting for high-voltage battery development. Its theoretical capacity is 148 mAh g⁻¹ and the practical reversible capacity is typically 100–125 mAh g⁻¹. More importantly, LiMn₂O₄ has an exceptionally high lithium-diffusion coefficient and a three-dimensional interstitial space that is able to withstand repeated lithium insertion and extraction. The spinel structure also possesses better tolerance to overcharge than layered oxides because lithium can be fully extracted from the tetrahedral 8a sites without immediate collapse of the oxygen framework. Since manganese is inexpensive and non-toxic, the manufacturing cost of a LiMn₂O₄-based high-voltage battery can be reduced substantially. In this thesis, commercial spinel LiMn₂O₄ powder was selected as the positive active material, while graphitic carbon was selected as the negative active material.
2. Experimental Techniques and Manufacturing Procedure
2.1 Raw materials
The manufacturing of LiMn₂O₄ high-voltage batteries requires controlled raw materials and well-characterized equipment. The principal raw materials used in this work are listed in Table 3.
| Material | Function |
|---|---|
| Spinel LiMn₂O₄ | Positive active material |
| Graphite | Negative active material |
| Conductive carbon black | Electronic conductivity enhancer |
| Poly(vinylidene fluoride) (PVDF) | Binder for the positive electrode |
| Water-based binder | Binder for the negative electrode |
| N-Methyl-2-pyrrolidone (NMP) | Solvent for the positive slurry |
| Aluminum foil | Positive current collector |
| Copper foil | Negative current collector |
| Porous polyolefin separator | Electronic separation between electrodes |
| LiPF₆-organic carbonate electrolyte | Ionic conductor |
| Prismatic steel can | Cell container |
All the raw powders were carefully dried and pre-treated before slurry preparation. In particular, the LiMn₂O₄ powder was selected with a particle-size distribution of 5–20 μm and a manganese content higher than 56 wt%. This level of purity can suppress self-discharge and hydrogen-evolution side reactions in the high-voltage battery.
2.2 General manufacturing flow of the high-voltage battery
The complete procedure can be divided into the positive-electrode line, the negative-electrode line, winding, assembly, electrolyte filling, formation, and grading. The successive steps of the electrode manufacturing process are:
- Weighing and dry mixing of the active material and conductive agent;
- Preparation of the polymer binder solution;
- Vacuum mixing of the slurry;
- Coating of the slurry onto an aluminum or copper foil;
- Drying and calendering of the electrode strip;
- Slitting, cutting, and welding of the tabs;
- Winding of the cell core;
- Inserting the core into the prismatic can and laser welding;
- Vacuum drying, electrolyte filling and formation;
- Sealing and final grading.
To guarantee uniform loading, the slurry viscosity was measured with a rotational viscometer and the slurry was passed through a colloid mill before coating. The coating machine was operated with a hot-air impingement drying system to prevent the formation of a dry outer skin that would trap solvent inside the coating. Double-side coating was used on both positive and negative current collectors, and the areal-density difference between the two sides was strictly controlled.
After coating and drying, the electrode strips were calendered by a roll press. The compaction density of the electrode is expressed as:
$$ \rho_{\text{compaction}} = \frac{m_{\text{coating}}}{A \cdot h_{\text{coating}}} $$
where \(m_{\text{coating}}\) is the total mass of the dried coating, \(A\) is the coating area and \(h_{\text{coating}}\) is the coating thickness after calendering.
The assembled cells were first welded by ultrasonic welding for the tabs, and then laser welding was employed to seal the steel can. Before electrolyte filling, the cells were thoroughly dried under vacuum at elevated temperature. Because water in a lithium-ion cell decomposes above approximately 1.2 V and causes gas evolution, the moisture content had to be minimized. The electrolyte filling operation was conducted in a glove box under a dry argon atmosphere, and the precise electrolyte mass was determined from the weight difference before and after filling.
3. Optimization of Key Manufacturing Parameters
3.1 Influence of active-material content on battery performance
The positive electrode of a lithium-ion battery is a composite film that contains active material, conductive additive, and polymeric binder. Conductive carbon black is necessary because LiMn₂O₄ has a rather low electronic conductivity, roughly \(10^{-4}\) to \(10^{-5}\) S cm⁻¹. The conductive agent builds a three-dimensional conductive network among the LiMn₂O₄ grains and reduces the contact resistance between the active material and the aluminum current collector. The binder provides mechanical integrity and helps the electrode accommodate volume changes during charge and discharge. If the contents of carbon black and binder are too high, the proportion of active material is reduced, so the capacity and energy density of the high-voltage battery decrease. If they are too low, the electrode has poor mechanical strength, high electronic resistance, and severe capacity fading.
To determine the optimum mixing formula, four batches of positive slurries were prepared with the same total solid mass and with LiMn₂O₄ contents of 90, 93, 96 and 98 wt%. The conductive additive and PVDF were adjusted accordingly. Ten-ampere-hour class prismatic cells were assembled with each formula, and their first discharge capacities and internal resistances are summarized in Table 4.
| LiMn₂O₄ content (wt%) | Discharge capacity at 0.2C (Ah) | Internal resistance (mΩ) |
|---|---|---|
| 90 | 8.9 | 1.1 |
| 93 | 9.6 | 1.2 |
| 96 | 10.2 | 1.4 |
| 98 | 10.3 | 1.8 |
It can be seen that the first discharge capacity increased markedly when the active-material content rose from 90 to 93 wt%, whereas the further increase from 96 to 98 wt% produced only a marginal capacity gain. Meanwhile, the internal resistance increased from 1.1 to 1.8 mΩ as the active-material content increased, because an insufficient amount of conductive carbon and binder worsens the electronic contacts both between the active particles and between the coating and the current collector.
Long-term cycling tests at a 1C rate were also performed for the four formulas. Table 5 reports the capacity retention after 200 cycles.
| LiMn₂O₄ content (wt%) | Capacity after 200 cycles (Ah) | Capacity retention (%) |
|---|---|---|
| 90 | 8.7 | 97.8 |
| 93 | 9.3 | 96.9 |
| 96 | 9.7 | 95.1 |
| 98 | 9.0 | 87.4 |
The electrode containing 98 wt% LiMn₂O₄ exhibited a rapid capacity fade because the conductive network and the binder phase were insufficient to maintain the electrode integrity upon repeated lithium insertion and extraction. The 96 wt% formula offered the best compromise among capacity, internal resistance and cycle stability, and was therefore selected as the optimum composition. This result demonstrates that the mixing formula is one of the most crucial factors in producing a reliable high-voltage battery.
3.2 Capacity-balance coefficient between positive and negative electrodes
In every lithium-ion cell, the negative electrode must provide a slightly larger reversible capacity than the positive electrode. If the positive capacity is higher than the negative capacity, lithium metal may be deposited on the graphite surface during charging. Continuous lithium plating can lead to dendrite growth, separator penetration and internal short-circuit, all of which create severe safety concerns in a large high-voltage battery. The capacity-balance coefficient is defined as:
$$ \gamma = \frac{\text{areal reversible capacity of the negative electrode}}{\text{areal reversible capacity of the positive electrode}} = \frac{\sigma_- \, w_- \, C_-}{\sigma_+ \, w_+ \, C_+} $$
where \(\sigma\) is the areal loading of the electrolyte coating, \(w\) is the active-material mass fraction, and \(C\) is the reversible specific capacity of the active material. In an ideal case, \(\gamma\) should be greater than 1.0 to avoid lithium plating. However, the manufacturing process always has unavoidable fluctuations in coating weight, so the design value of \(\gamma\) must be sufficiently large to guarantee that the local balance factor remains above 1.0 for every point on the electrode. In this production line, the coating deviation was measured to be about ±2\%, which sets a minimum design value of approximately 1.04.
To study the influence of \(\gamma\), prismatic batteries were assembled with capacity-balance coefficients of 1.02, 1.05, 1.10 and 1.20. The discharge capacity of the batteries is compared in Fig. 1 of the original thesis, and the general trend is shown in Table 6.
| Capacity-balance coefficient γ | 0.2C discharge capacity (Ah) | Overcharge behaviour at 3C/4.6 V | Maximum temperature in nail penetration (°C) | Maximum temperature in short circuit (°C) |
|---|---|---|---|---|
| 1.02 | 9.4 | Vent occurred | ~95 | ~82 |
| 1.05 | 10.1 | No fire, no explosion | ~68 | ~60 |
| 1.10 | 10.2 | No fire, no explosion | ~65 | ~58 |
| 1.20 | 9.5 | No fire, no explosion | ~64 | ~57 |
When the balance coefficient was too low, such as 1.02, the cell delivered a lower capacity because graphite particles consumed part of the lithium inventory during the formation of the solid-electrolyte interphase (SEI), and excessive lithium insertion could result in metallic lithium deposition under overcharge. The thermal-runaway tests showed that this battery generated much more heat and had the highest risk. When the balance coefficient was increased to 1.05–1.10, the capacity was maximized and the safety behaviour was acceptable. If the balance coefficient was raised to 1.20, the excess graphite increased the total electrode thickness unnecessarily and made the cell package too tight, which hindered electrolyte penetration and reduced the discharge capacity. Therefore, the optimum range of the capacity-balance coefficient was determined to be 1.05–1.10 for this high-voltage battery process.
3.3 Electrode compaction density and assembly tightness
The compaction density of an electrode determines the porosity, the tortuosity and the electrical conductivity of the coating. A proper compaction density is necessary to obtain a high volumetric energy density while maintaining sufficient pore space for electrolyte wetting. In this work, the graphite negative electrode was first fixed at its optimum density while the LiMn₂O₄ positive electrode was calendered to different compaction densities. The assembly success and the cell capacity were then evaluated. Table 7 gives the assembly yield for different positive compaction densities.
| Positive compaction density (g cm⁻³) | Assembled cells | Short-circuited cells | Assembly success rate (%) |
|---|---|---|---|
| 2.4 | 20 | 6 | 70 |
| 2.7 | 20 | 2 | 90 |
| 3.0 | 20 | 0 | 100 |
| 3.2 | 20 | 0 | 100 |
When the compaction density was as low as 2.4 g cm⁻³, the electrode was too thick and the wound electrode assembly was scratched by the steel can during insertion, which produced many short-circuited cells. When the compaction density reached 3.0 g cm⁻³, the electrodes had suitable thickness and the assembly yield reached 100\%.
Figure 3 in the original thesis shows the discharge curves of cells prepared at different positive densities. The discharge capacity increased when the density changed from 2.4 to 3.0 g cm⁻³, because the contact among LiMn₂O₄ particles was improved. When the density was increased further to 3.2 g cm⁻³, the rate capability decreased, especially at high discharge rates, because the electrode pores became too small for rapid electrolyte diffusion. The optimum compaction densities were therefore determined to be 3.0 g cm⁻³ for the LiMn₂O₄ positive electrode and 1.5 g cm⁻³ for the graphite negative electrode.
The assembly tightness is another important structural parameter of a prismatic high-voltage battery. It is defined as:
$$ K_{\text{tightness}} = \frac{n_+ h_+ + n_- h_- + n_{\text{sep}} h_{\text{sep}}}{t_{\text{inner}}} $$
where \(n\) and \(h\) are the number and thickness of each component layer and \(t_{\text{inner}}\) is the internal thickness of the cell can. From the optimized electrode densities, the suitable assembly tightness was found to be in the range of 0.85–0.95. Excessive tightness makes electrolyte filling difficult and leads to poor wetting, whereas insufficient tightness increases the internal resistance and can cause electrode displacement during cycling.
3.4 Electrolyte filling amount
The electrolyte must completely fill the pores of the positive electrode, the negative electrode and the separator. If the electrolyte amount is insufficient, some active particles are not wetted by the electrolyte and the discharge capacity is low. In addition, a lean electrolyte condition promotes concentration polarization and increases the internal resistance. If the electrolyte amount is excessive, the high-voltage battery may leak, and during open-formation the surplus electrolyte can corrode the production equipment. Therefore, the electrolyte volume should be optimized not only from an electrochemical viewpoint, but also from an industrial-manufacturing viewpoint.
A series of prismatic cells was produced with electrolyte filling amounts of 6.5, 7.0, 7.5, 8.0, 8.5 and 9.0 g. The discharge capacity and internal resistance of these cells are presented in Table 8.
| Electrolyte amount (g) | First discharge capacity (Ah) | Internal resistance (mΩ) |
|---|---|---|
| 6.5 | 9.1 | 2.0 |
| 7.0 | 9.8 | 1.8 |
| 7.5 | 10.2 | 1.5 |
| 8.0 | 10.4 | 1.3 |
| 8.5 | 10.4 | 1.3 |
| 9.0 | 10.4 | 1.2 |
When the electrolyte amount was 7.5 g, the capacity was already close to the saturated value. Further addition of electrolyte beyond 8.0 g produced only marginal capacity improvement and little change in internal resistance. A capacity-distribution experiment was conducted on a larger number of cells, and the results are summarized in Table 9.
| Electrolyte amount (g) | Capacity < 9.5 Ah (%) | Capacity 9.5–10.2 Ah (%) | Capacity > 10.2 Ah (%) |
|---|---|---|---|
| 7.0 | 18 | 64 | 18 |
| 7.5 | 4 | 31 | 65 |
| 8.0 | 2 | 17 | 81 |
| 8.5 | 1 | 12 | 87 |
Although a larger filling amount slightly improved the high-capacity yield, it was also observed that some cells filled with 8.5 g of electrolyte showed slight electrolyte bleeding during the open formation step. In view of mass-production reliability, the optimal electrolyte amount for this high-voltage battery was set to 8.0 g per 10-Ah cell, which gives a high qualification rate and no significant leakage problem.
3.5 Formation schedule
The formation process is the first charge after electrolyte filling. During formation, the SEI film is established on the graphite surface. A well-formed SEI film prevents further reductive decomposition of electrolyte and lithium-solvent co-intercalation into graphene layers, thus determining the coulombic efficiency, rate capability, safety and service life of the high-voltage battery. If the formation current is too high, the SEI film is non-uniform and porous; if the current is too low, the formation time becomes excessively long. Furthermore, gas generation during SEI formation is unavoidable, and it can cause electrode deformation if not appropriately released. In this work, the cells were therefore subjected to open formation and then sealed by a steel ball after degassing.
Three formation schedules were compared, as listed in Table 10.
| Formation process | Description |
|---|---|
| A | Charge at 0.05C to 4.2 V |
| B | Charge at 0.05C for 2 h, then at 0.1C to 4.2 V |
| C | Charge at 0.02C for 2 h, then at 0.1C to 4.2 V |
After formation, all cells were discharged and their capacities, internal resistances and first-cycle coulombic efficiencies were measured. The general comparison is shown in Table 11.
| Formation process | Average capacity (Ah) | Internal resistance (mΩ) | First-cycle Coulombic efficiency (%) |
|---|---|---|---|
| A | 9.9 | 1.7 | 82.5 |
| B | 10.1 | 1.5 | 85.3 |
| C | 10.3 | 1.4 | 87.6 |
Process C, which started with a very small 0.02C charging current, produced the highest discharge capacity and the lowest internal resistance. The small current allowed the SEI film to grow gradually and uniformly on the graphite surface, and allowed gas bubbles generated in the initial stage to escape gently from the open cell. The first-cycle Coulombic efficiency was also the highest, indicating that less lithium was consumed by irreversible side reactions. The cycle-life test further confirmed that the cells formed by process C had a slightly better capacity retention after 300 cycles. The final adopted formation schedule was therefore:
- Charge at 0.02C for 2 h;
- Then charge at 0.1C until the cell voltage reached 4.2 V;
- Rest, degas and seal;
- Perform a full charge/discharge grading cycle.
This formation schedule effectively reduces gas-swelling defects and improves the activation efficiency of the active materials in the high-voltage battery.
3.6 Performance of the optimized high-voltage battery
Using the optimized process parameters, the 10-Ah class prismatic LiMn₂O₄ high-voltage battery exhibited excellent discharge performance. The test results are summarized in Table 12.
| Parameter | Value |
|---|---|
| 0.2C discharge capacity | 10.6 Ah |
| 0.5C discharge capacity | 10.5 Ah |
| 1C discharge capacity | 10.4 Ah |
| 2C discharge capacity | 10.2 Ah |
| Internal resistance | ~1.3 mΩ |
| Self-discharge rate | ~0.2\% per day |
| Cycle life at 1C | > 300 cycles |
Safety tests, including overcharge, crushing, external short-circuit and nail penetration, were also performed. In every test, the battery did not catch fire or explode, which verified that the optimized cell design has an acceptable level of abuse tolerance and satisfies the requirements of a modern high-voltage battery for electric traction.
4. Design and Fabrication of a Large-Capacity LiMn₂O₄ High-Voltage Battery
4.1 Design specifications
Based on the optimized manufacturing technology described above, a large-capacity prismatic LiMn₂O₄ high-voltage battery was designed for electric-vehicle applications. The primary design objective was to combine high capacity with high power capability and excellent abuse tolerance. The design targets are listed in Table 13.
| Parameter | Target value |
|---|---|
| Nominal capacity | 10 Ah |
| Nominal voltage | 3.7 V |
| Internal resistance | ≤ 1.5 mΩ |
| Specific power at high-rate discharge | ≥ 800 W kg⁻¹ |
| Specific energy | ≥ 90 Wh kg⁻¹ |
| Cycle life at 1C, 100\% DOD | ≥ 500 cycles |
| Safety | No fire, no explosion in abuse tests |
4.2 Crystal structure and morphology of the active material
The spinel LiMn₂O₄ powder was characterized by X-ray diffraction. The XRD pattern exhibited the characteristic diffraction peaks of cubic spinel LiMn₂O₄ at (111), (311) and (400), with the expected (111) peak being the strongest. No impurity peaks were observed, confirming that the powder had a well-crystallized spinel structure. Scanning electron microscopy of the powder revealed irregular block-shaped particles with a relatively homogeneous particle-size distribution. Some fine particles adhered to the surfaces of larger particles, which is beneficial for increasing the contact area and the electronic conduction in the electrode coating.
4.3 Determination of the cell capacity and electrode loading
The design of a battery is usually an inverse process: the outer dimensions of the cell are fixed first, and the electrode dimensions are then calculated according to the target capacity. The design capacity should be moderately larger than the nominal capacity to compensate for irreversible capacity loss during formation and to guarantee that the rated capacity can be delivered throughout the service life. The design capacity \(C_d\) is related to the rated capacity \(C_r\) by:
$$ C_d = \frac{C_r}{\eta} $$
where \(\eta\) is the design margin factor, typically 0.85–0.95 for a new high-voltage battery. In this work, the design capacity was selected to be 11 Ah for a rated capacity of 10 Ah. The required mass of the positive active material is:
$$ m_+ = \frac{C_d}{C_{+,\text{specific}}} $$
where \(C_{+,\text{specific}}\) is the practical specific capacity of the LiMn₂O₄ cathode. For the negative electrode, the mass of graphite is:
$$ m_- = \frac{C_d}{C_{-,\text{specific}}} \times \gamma $$
where \(C_{-,\text{specific}}\) is the practical reversible specific capacity of the graphite anode and \(\gamma\) is the capacity-balance coefficient. The total coating area of the positive electrode is then:
$$ A_+ = \frac{m_+}{a_+} $$
where \(a_+\) is the areal loading of the positive electrode. The length of the positive electrode is obtained from:
$$ L_+ = \frac{A_+}{W_+} $$
and the negative electrode length is chosen to be slightly longer than the positive electrode:
$$ L_- = L_+ + L_{\text{overhang}} $$
The multi-tab or multi-roll design was adopted so that the current distribution is uniform over the large electrode. A multi-roll structure was used in the prismatic can to reduce the electronic path and thereby lower the internal resistance of the large high-voltage battery. The separator was wound together with the electrodes in the order: positive electrode / separator / negative electrode / separator. The winding was carefully controlled so that the negative electrode completely covered the positive electrode at both the leading edge and the trailing edge, preventing lithium plating at the electrode edges.
4.4 Fabrication of the electrodes and assembly
For the positive electrode, LiMn₂O₄, carbon black and PVDF were dispersed in NMP according to the optimized proportion. The slurry was coated onto 20-μm-thick aluminum foil. After drying, the electrode was calendered to the optimized compaction density of 3.0 g cm⁻³. Aluminum tabs were welded by ultrasonic welding.
For the negative electrode, graphite, carbon black and a water-based binder were mixed with deionized water. The slurry was coated onto 12-μm-thick copper foil and dried. The negative electrode was calendered to a compaction density of 1.5 g cm⁻³. Nickel tabs were welded onto the bare copper foil at the designated positions, and the exposed foil was covered with insulating tape.
The electrode strips were then wound into a jelly-roll core by an automatic winding machine. The winding tension was controlled carefully, because too high a tension makes the core too tight and hinders electrolyte wetting, while too low a tension leads to a loose core with high resistance and possible electrode shifting. The finished core was inserted into the prismatic steel can. After the negative tabs were welded to the can and the positive tabs to the cap, the can was sealed by laser welding. The welded cells were dried under vacuum and then transferred directly to the argon-filled glove box for electrolyte filling. After filling, the cells were allowed to rest for a sufficient period to ensure full wetting.
4.5 Electrochemical properties of the large high-voltage battery
The first charge/discharge curves of the large-capacity LiMn₂O₄ high-voltage battery are shown in Fig. 1 in the original thesis. At room temperature, the battery was charged at constant current to 4.2 V, followed by constant-voltage charging until the current decreased to a small cut-off value. It was then discharged at constant current to 3.0 V. The first charge capacity was approximately 11.2 Ah, and the first discharge capacity was about 10.8 Ah, corresponding to a first-cycle Coulombic efficiency of nearly 96\%. The high efficiency implies that the SEI film was well formed and the irreversible capacity loss was small.
The internal resistance of the battery was measured with a four-probe AC impedance tester at the fully charged state. The measured value was about 1.2 mΩ, which satisfies the design requirement of ≤ 1.5 mΩ. A low internal resistance is important for a high-voltage battery used in electric vehicles, because it enables high-current discharge with less heat generation and less voltage drop.
The rate capability was evaluated at discharge currents of 0.2C, 0.5C, 1C, 2C and 5C. All discharges were performed at room temperature after an identical charging procedure. The discharge capacities at different rates are summarized in Table 14.
| Discharge rate | Discharge capacity (Ah) | Capacity relative to 0.2C (%) | Median voltage (V) |
|---|---|---|---|
| 0.2C | 11.0 | 100 | 3.85 |
| 0.5C | 10.9 | 99.0 | 3.80 |
| 1C | 10.7 | 97.2 | 3.72 |
| 2C | 10.5 | 95.5 | 3.60 |
| 5C | 9.9 | 90.0 | 3.35 |
At a 5C discharge rate, the large high-voltage battery still delivered 9.9 Ah, which is equivalent to about 90\% of the 0.2C capacity. The excellent rate capability is attributed to the three-dimensional lithium diffusion channels in spinel LiMn₂O₄, the optimized porosity of the electrode coatings, the low internal resistance of the multi-roll structure, and the adequate electrolyte amount.
The specific power \(P_s\) and specific energy \(E_s\) of the high-voltage battery can be written as:
$$ E_s = \frac{\bar{V} \times Q}{m_{\text{cell}}} $$
$$ P_s = \frac{\bar{V} \times I}{m_{\text{cell}}} $$
where \(Q\) is the discharge capacity, \(I\) is the discharge current, \(\bar{V}\) is the average discharge voltage, and \(m_{\text{cell}}\) is the total mass of the cell. The mass of the large prismatic battery was about 380 g. Therefore, the specific energy reached approximately 100 Wh kg⁻¹ at the 1C discharge rate, and the specific power reached about 850 W kg⁻¹ at the 5C discharge rate. Both values satisfy the design targets and clearly demonstrate the suitability of this LiMn₂O₄ high-voltage battery for electric-vehicle applications.
4.6 Storage characteristics and charge retention
The self-discharge of the large high-voltage battery was evaluated by storing the fully charged cell at room temperature for 30 days. After storage, the cell was discharged at the 0.2C rate. The residual discharge capacity was measured to be 9.9 Ah, which is 90\% of the nominal capacity, corresponding to an average self-discharge rate of about 0.3\% per day. The cell was then recharged and discharged again to evaluate the capacity-recovery ability. The recovered capacity was 10.4 Ah, corresponding to about 95\% of the nominal capacity. The excellent charge retention and capacity recovery indicate that the high-voltage battery has only small side reactions during storage.
4.7 Cycle life
Electric-vehicle batteries are subjected to frequent charge/discharge cycling, so the cycle life is a critical parameter. The large LiMn₂O₄ high-voltage battery was cycled at a 1C charge/discharge rate with a charge cut-off voltage of 4.2 V and a discharge cut-off voltage of 3.0 V. After 500 cycles, the discharge capacity remained above 9.2 Ah, corresponding to about 92\% of the initial capacity and about 92\% of the nominal capacity. The battery demonstrated good capacity retention and stable coulombic efficiency over the entire cycling test, confirming that the optimized manufacturing process successfully suppressed the capacity fading that is commonly observed in LiMn₂O₄ electrodes. The cycling stability is particularly important for long-life high-voltage battery packs in electric vehicles.
4.8 Safety tests
For vehicle applications, the safety of a high-voltage battery is the most important consideration. The large LiMn₂O₄ high-voltage battery was tested according to the general safety standards for traction lithium-ion batteries. The test items and results are summarized in Table 15.
| Abuse test | Test condition | Requirement | Result |
|---|---|---|---|
| Overcharge | 3C charge to 4.6 V | No fire, no explosion | Pass |
| External short circuit | External resistance < 5 mΩ | No fire, no explosion | Pass |
| Nail penetration | Steel nail penetration through the cell | No fire, no explosion | Pass |
| Hot-oven exposure | 150 °C for 30 min | No fire, no explosion | Pass |
The excellent abuse tolerance arises from the intrinsically stable spinel structure, the optimized capacity-balance coefficient, the robust SEI film formed under the mild formation schedule, and the proper electrolyte-to-electrode ratio. Even in the nail-penetration test, only a mild temperature rise without fire or explosion was observed. This demonstrates that the manufacturing process described in this work can produce a high-voltage battery that meets the safety requirements for electric vehicles.
5. Conclusions
In this work, the key manufacturing parameters that control the performance of LiMn₂O₄ high-voltage batteries were systematically studied, and a 10-Ah class prismatic power battery was successfully designed and fabricated using the optimized process. The main conclusions are as follows:
- Spinel LiMn₂O₄ with a particle size of 5–20 μm and a manganese content greater than 56 wt\% is an appropriate positive active material for high-voltage lithium-ion power batteries.
- The positive electrode composition significantly influences the discharge capacity, internal resistance and cycle stability. The optimal LiMn₂O₄ content was determined to be 96 wt\%, which gives a balanced combination of high capacity, acceptable resistance and stable cycling.
- The capacity-balance coefficient between the positive and negative electrodes should be designed in the range of 1.05–1.10. Too low a coefficient causes lithium plating and safety risk, while too high a coefficient reduces the energy density and increases the electrode thickness.
- The optimum compaction density was found to be 3.0 g cm⁻³ for the LiMn₂O₄ positive electrode and 1.5 g cm⁻³ for the graphite negative electrode. The preferred assembly tightness was 0.85–0.95.
- The electrolyte filling amount should be carefully matched to the porosity of the electrode stack. For the 10-Ah high-voltage battery, the optimum electrolyte amount was approximately 8.0 g per cell, which ensures high capacity, low internal resistance, high qualification yield and no unacceptable leakage risk.
- A two-stage formation schedule, starting with a 0.02C charge and then continuing at 0.1C to 4.2 V, was shown to produce a better SEI film, greater first-cycle Coulombic efficiency, lower internal resistance and a slightly longer cycle life than simpler constant-current schedules.
- The large-capacity LiMn₂O₄ high-voltage battery delivered more than 10 Ah at 0.2C, a 5C capacity retention of about 90\%, a specific energy close to 100 Wh kg⁻¹, a specific power above 800 W kg⁻¹, a storage capacity retention of 90\% after 30 days, and stable cycling for more than 500 cycles. The battery also passed overcharge, external short-circuit, nail-penetration and hot-oven safety tests.
The overall results confirm that the optimized manufacturing technology is capable of producing a prismatic LiMn₂O₄ high-voltage battery with excellent electrochemical performance and safety, making it a very attractive power source for electric vehicles, hybrid electric vehicles and other high-power energy-storage applications. Further research should continue to improve the high-temperature cycle stability of the spinel cathode, reduce the production cost of the large-format cells, and develop even more reliable battery-management strategies for traction systems.